Forged ball valve components
We forge the body.
You build the valve.
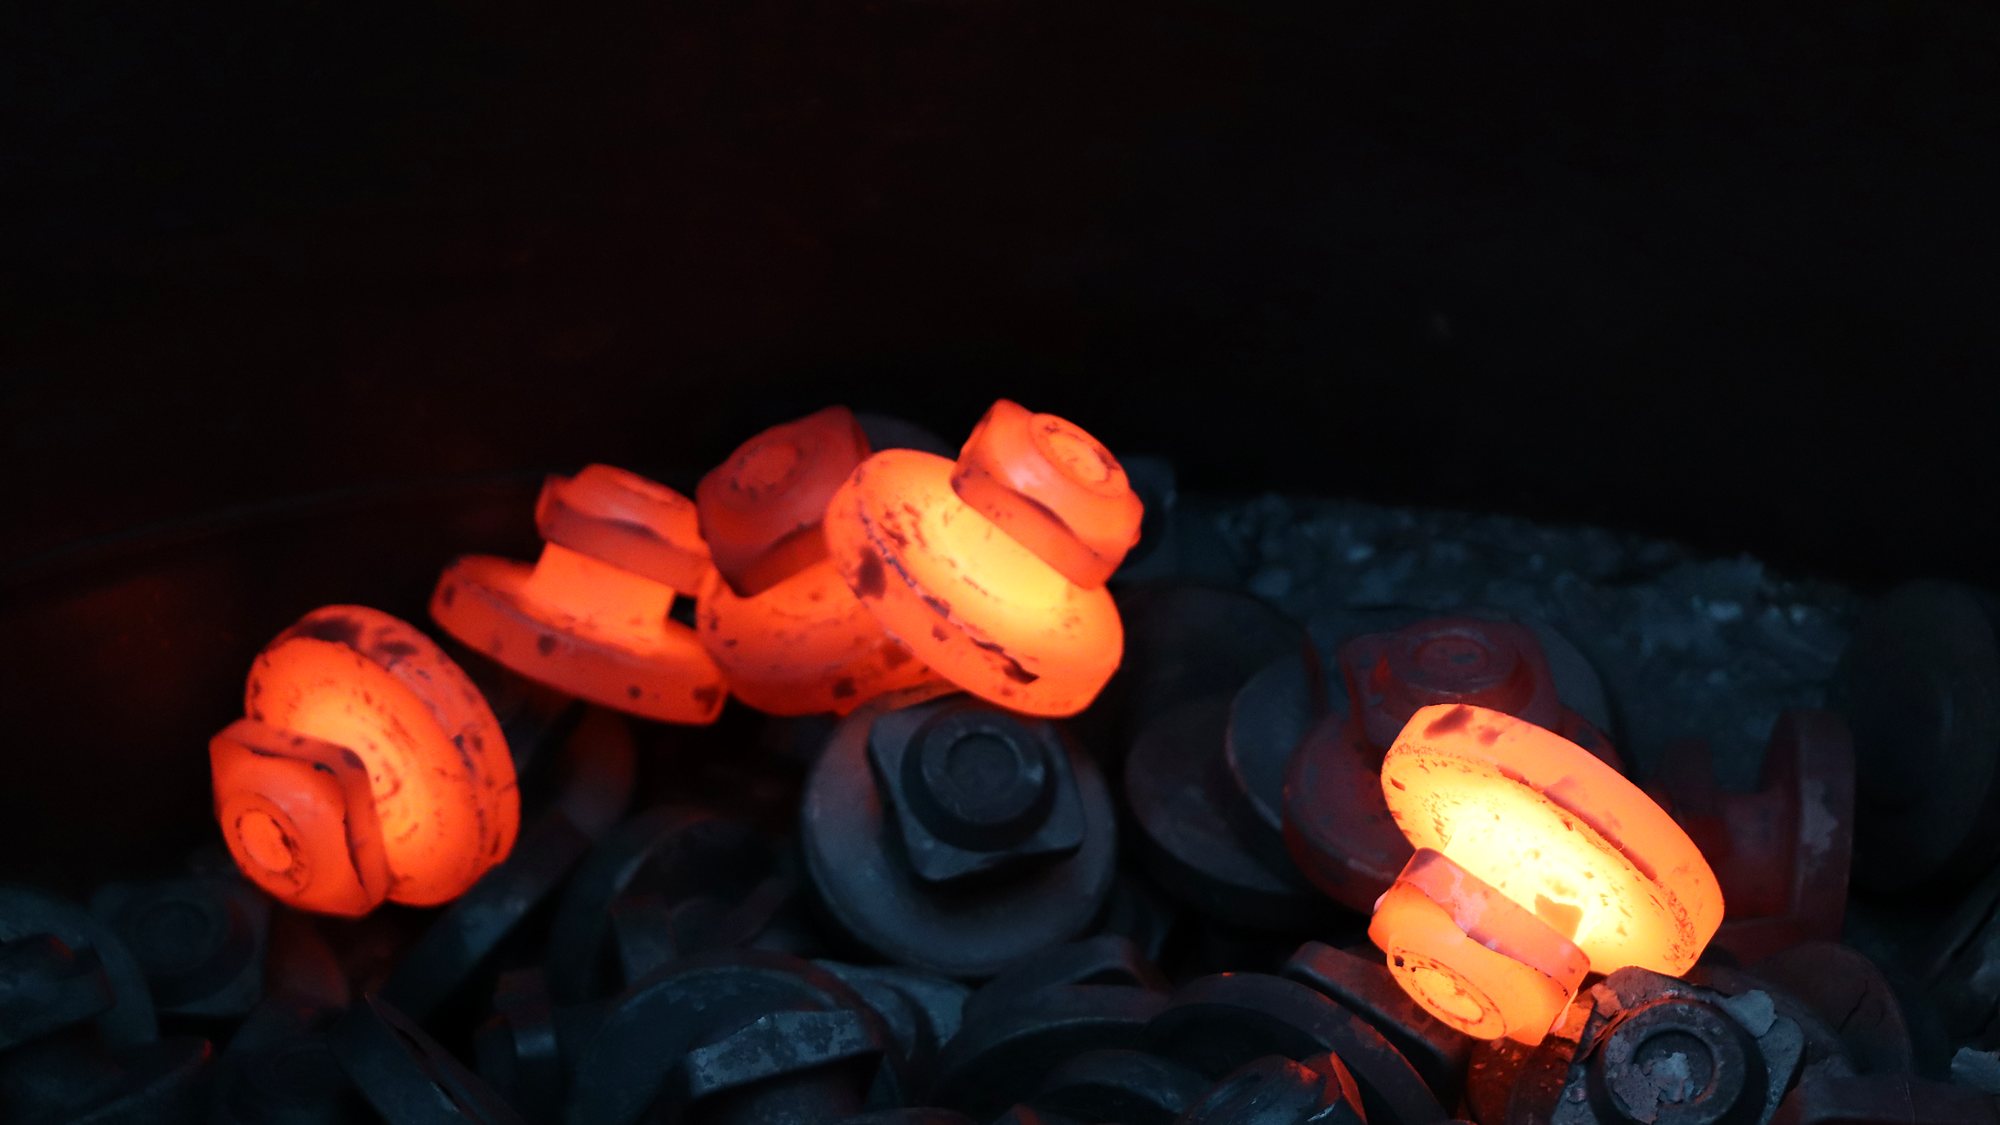
One-piece closed-die forgings in carbon and stainless steel for valve manufacturers worldwide. We forge, heat treat, blast and machine on our own site.
Product programme
Nine nominal sizes,
drawn to scale.
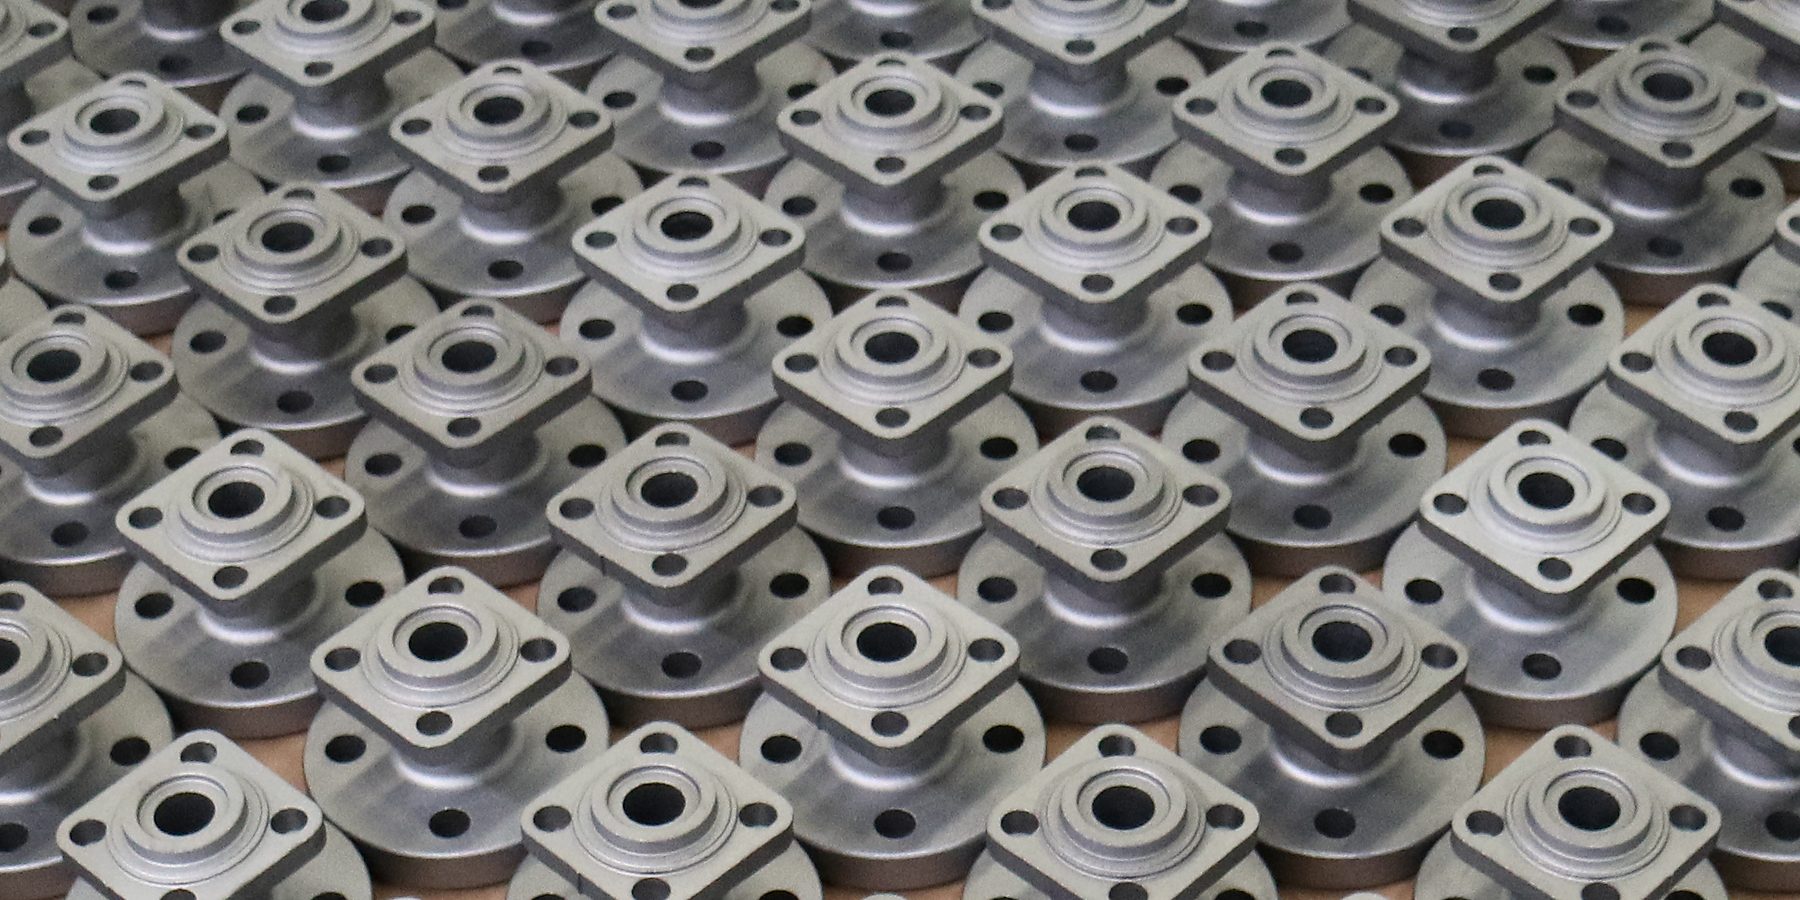
Ball valve bodies from DN15 to DN100 — NPS ½″ to 4″ — rated up to Class 300 (300 lb), and any other forging you can send us a drawing for. The bores on the right are at true relative size to each other.
| Grade | Standard | Size | Service |
|---|---|---|---|
| A105 carbon steel | ASTM A105 | DN15 – DN100 NPS ½″ – 4″ | Oil, gas and water |
| 304 stainless | ASTM A182 F304 | DN15 – DN100 NPS ½″ – 4″ | General industrial |
| 316 stainless | ASTM A182 F316 | DN15 – DN100 NPS ½″ – 4″ | Corrosive media |
| Custom grades | To customer spec | On request | To drawing |
Typical components
- Ball valve bodies, forged in one piece. This is what the plant is built around.
- Bonnets, caps, end connections and connecting flanges.
- Special parts made from scratch, die included, to your drawing.
Supply condition
- Forged blanks (optional blasted to ISO 8501-1 Sa 2½).
- Rough machined blanks (optional blasted to ISO 8501-1 Sa 2½).
- Finish machined parts (optional blasted to ISO 8501-1 Sa 2½).
Capacity and facilities
Built for repeat
series work.
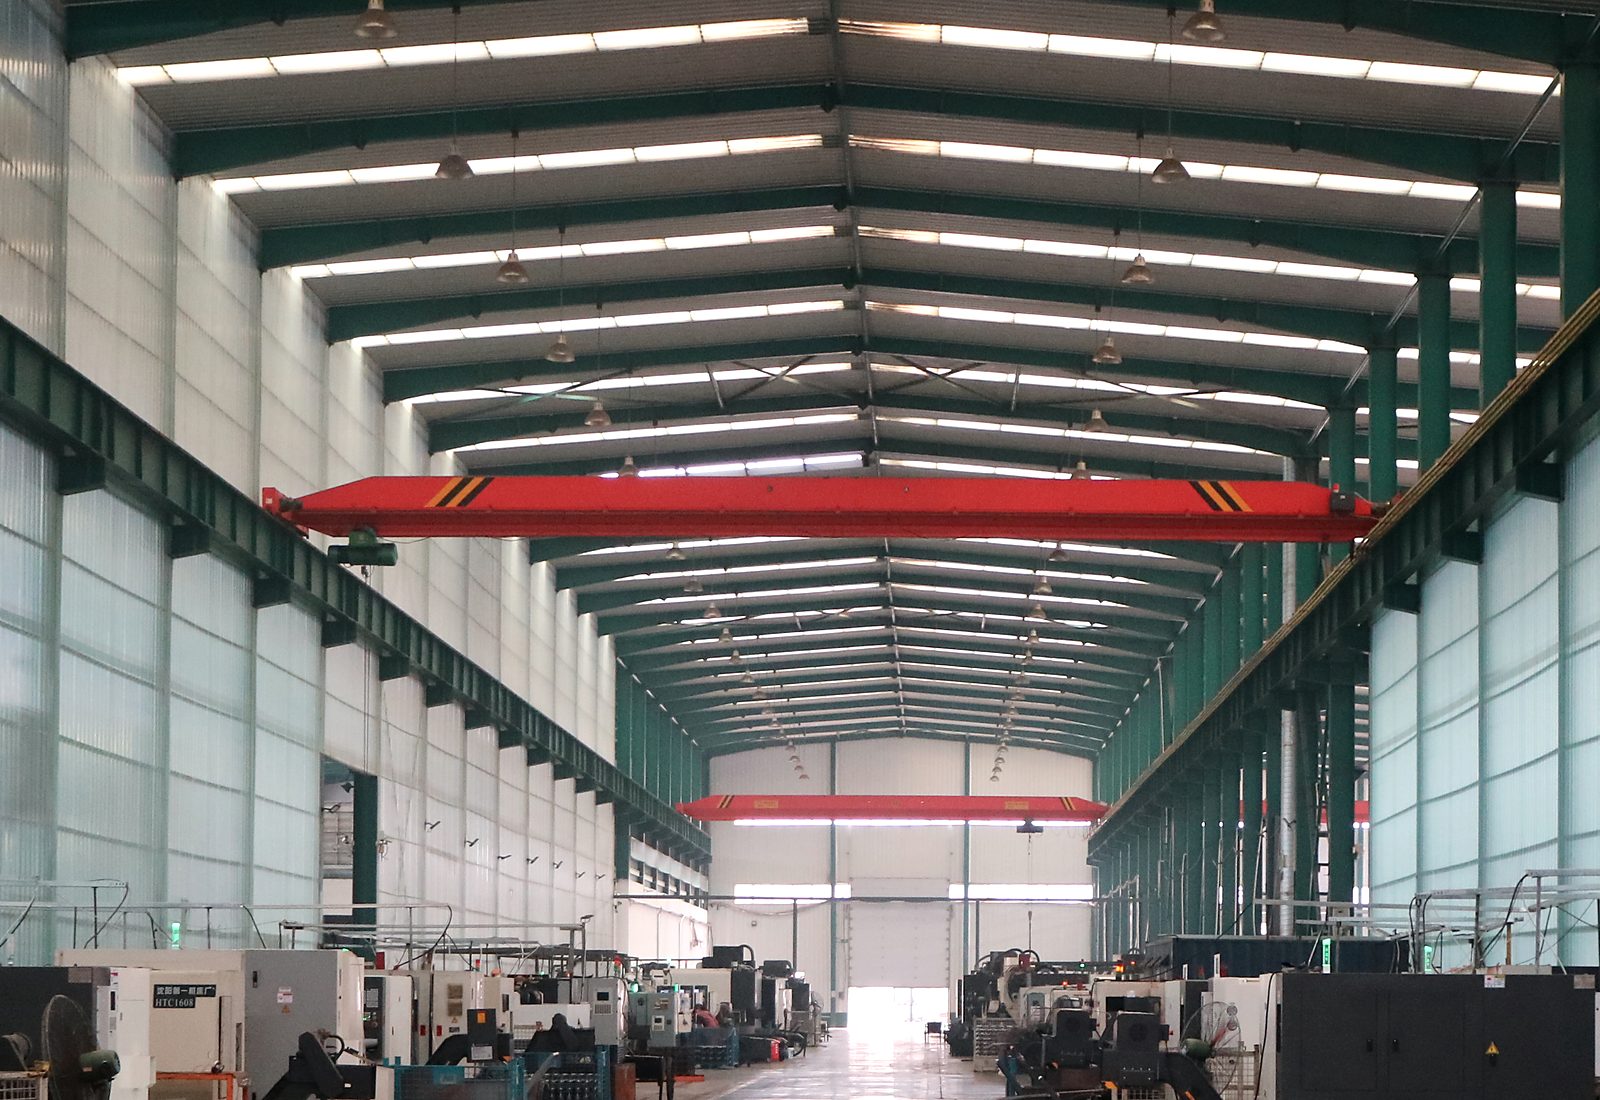
Eight closed-die forging lines and more than a hundred and ten CNC machines on one site, with the presses and the automation to hold one shape run after run.
From drawing to delivery
Seven stages,
in order.
Every part follows the same route from a customer CAD drawing to a certified forging, ready for machining.
-
1Drawing and DFM review
We review the drawing and the specification, say what would make the part easier to forge, and agree a tooling plan.
-
2Die design and simulation
Dies are designed and cut here on 3D CAD/CAM, with the forming step simulated before steel is committed.
-
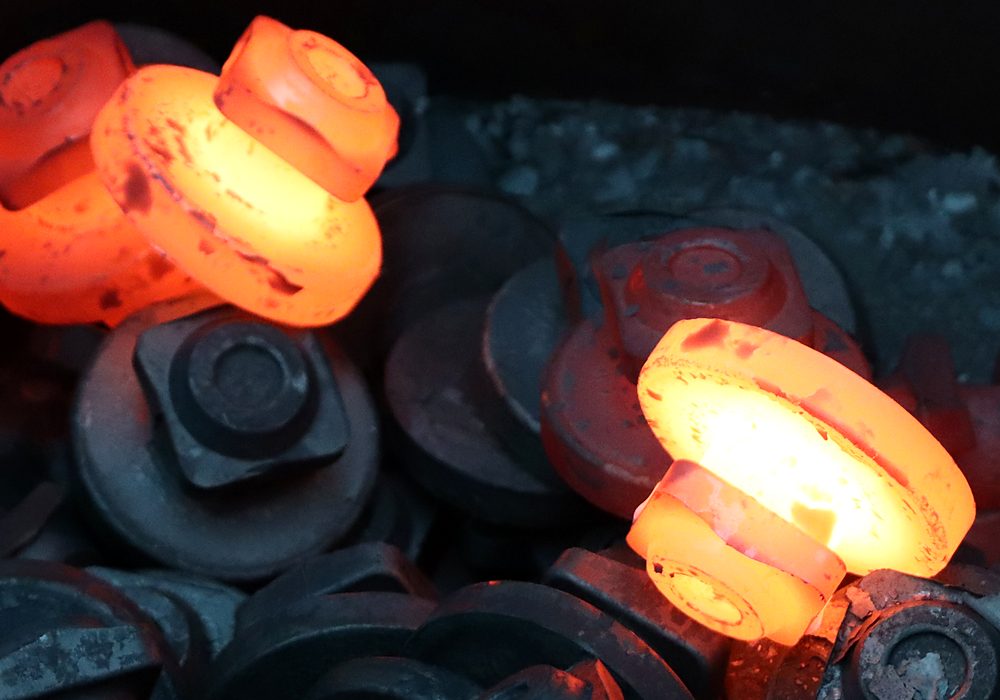
3Closed-die forging
Certified billet is heated and forged on 315 to 2,500 t servo presses with programmable forming energy.
-
4Heat treatment
Normalising, solution annealing or quench and temper, to suit the grade and the properties called for.
-
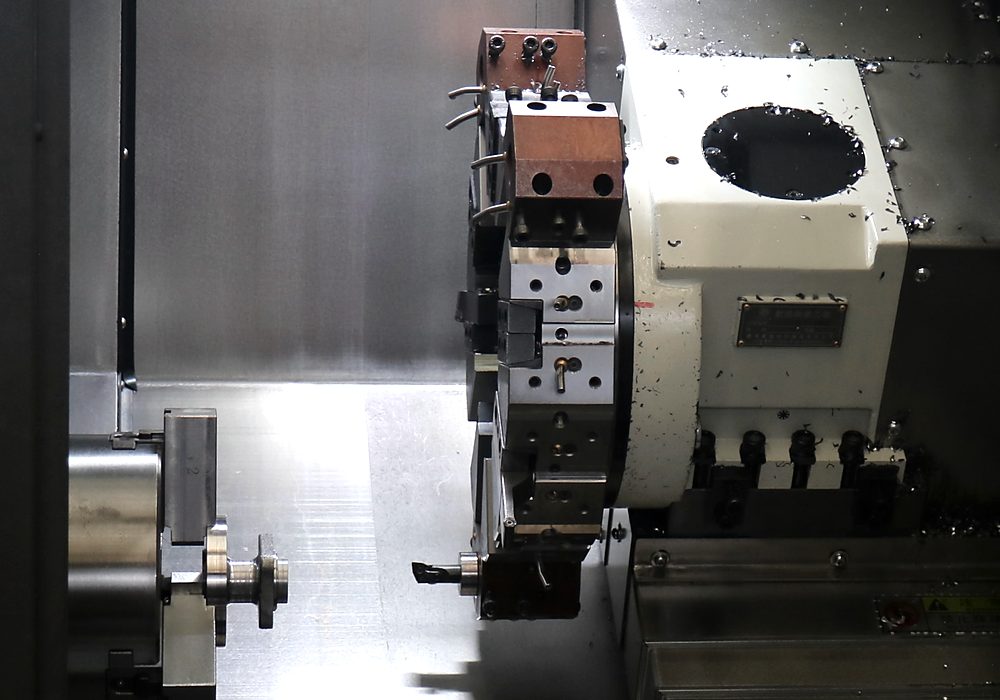
5CNC machining
Rough or finish turning and milling on 90+ CNC lathes and 22 machining centres, to the stock you specify.
-
6Blasting to Sa 2½
Shot blasting to ISO 8501-1 Sa 2½ removes all mill scale and leaves a clean, near white surface.
-
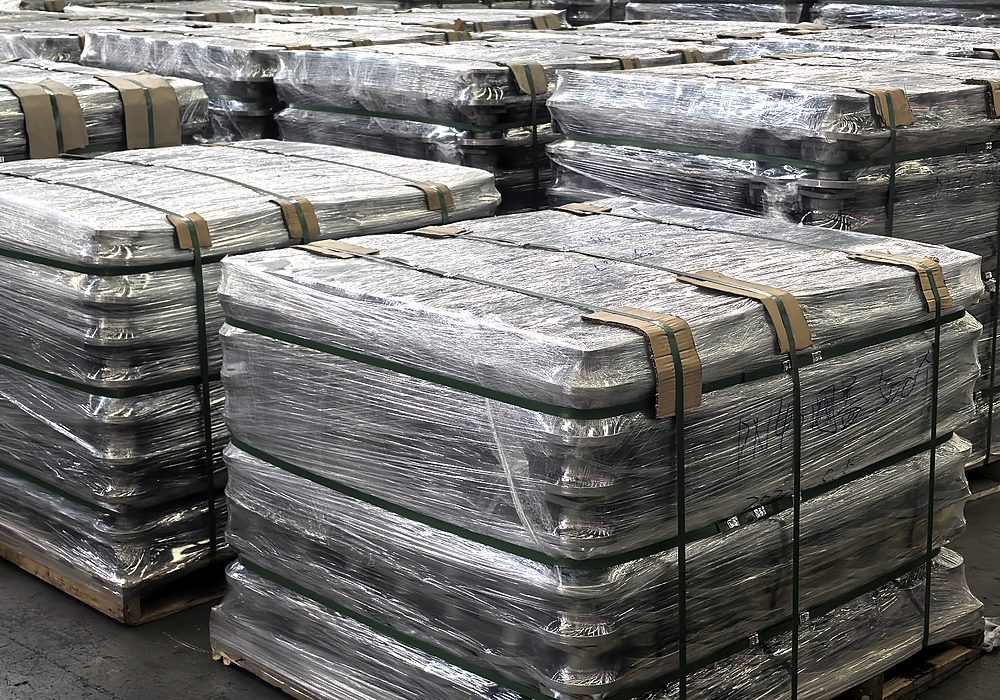
7Inspection, packing and export
Dimensions, hardness and material are verified, the EN 10204 3.1 papers are issued, and parts are preserved and packed for export.
Certification
Certified, and
checkable.
The certificate itself, with the numbers your QA department needs to check it against the register.
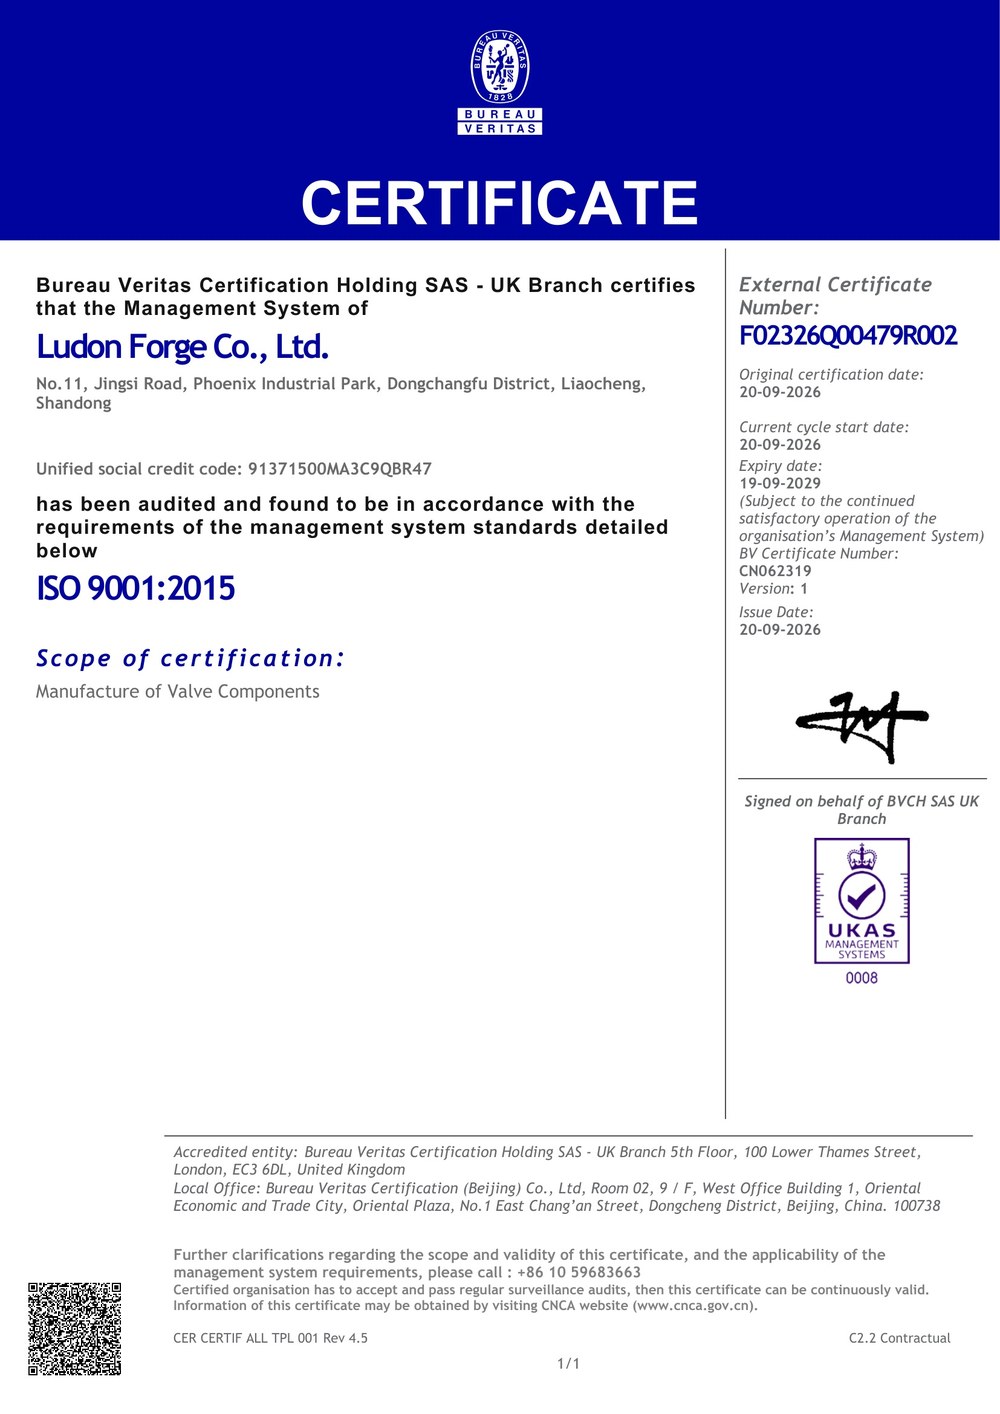
ISO 9001:2015
- Registrar
- Bureau Veritas Certification Holding SAS – UK Branch
- Certificate
- F02326Q00479R002 · BV CN062319
- Valid
- 20-09-2026 – 19-09-2029
- Accreditation
- UKAS 0008
EN 10204 3.1 material certificate with every heat, and a first article report on any new item.
Insights
What we know
about forging.
Technical notes for engineers and buyers specifying forged pressure-containing components.
Technical guide
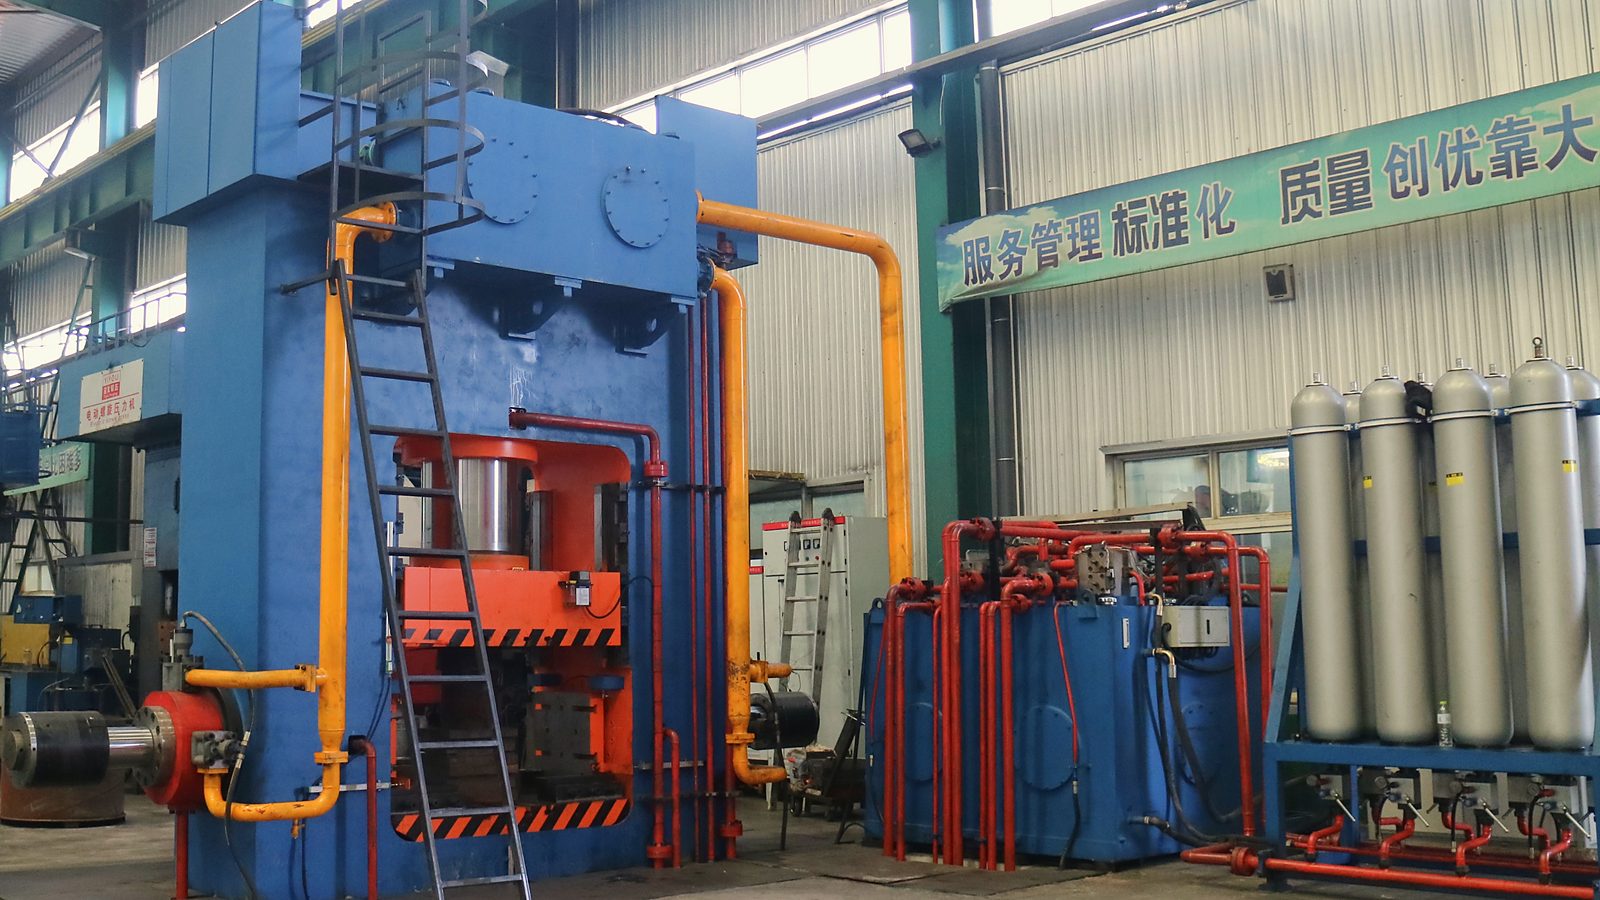
The advantages of closed die forging
What the process does to metal, why grain flow decides a pressure boundary, and where forging beats casting and bar machining — with an honest note on where it does not.
Read the guide →
Our process
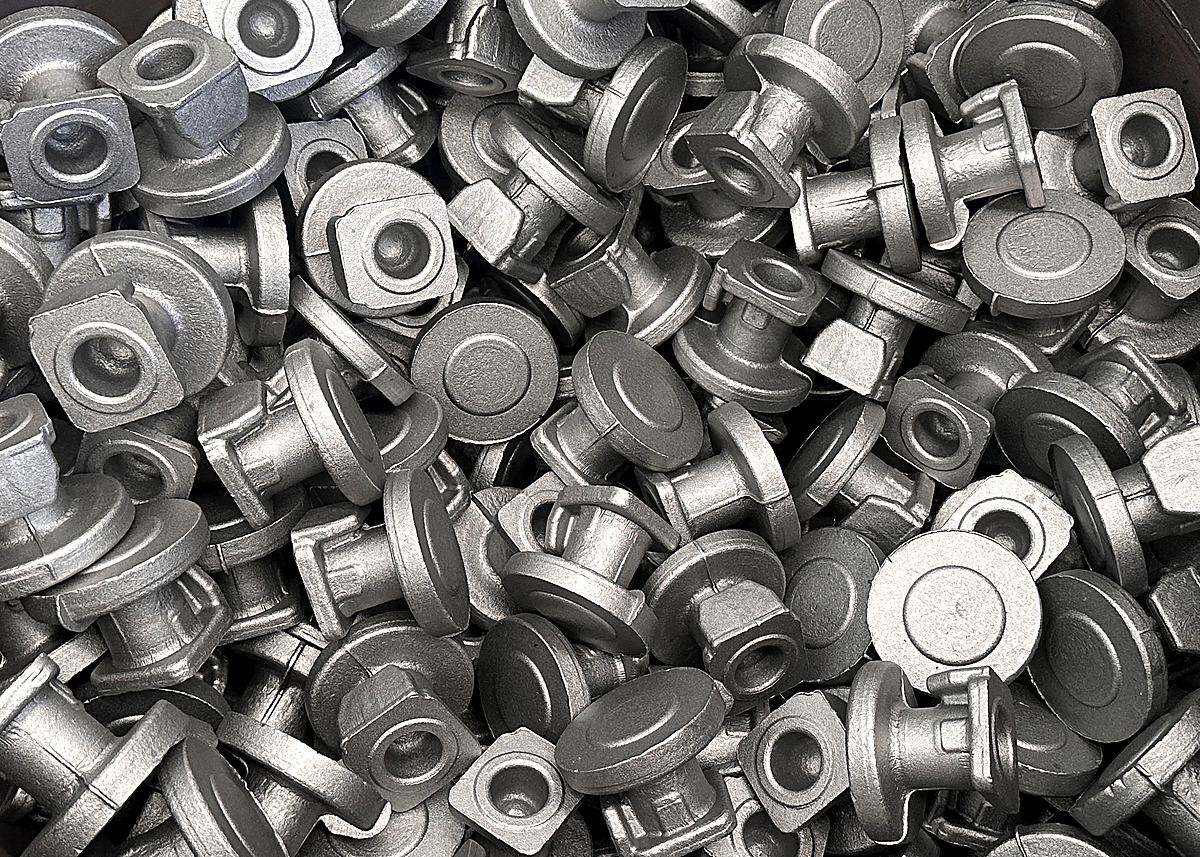
One-piece multi-directional forging
How forming a valve body from several directions in one heat removes the weld, carries grain flow into the stem boss and forms the bore instead of drilling it.
Read the note →
Enquiries
Send us
your drawing.
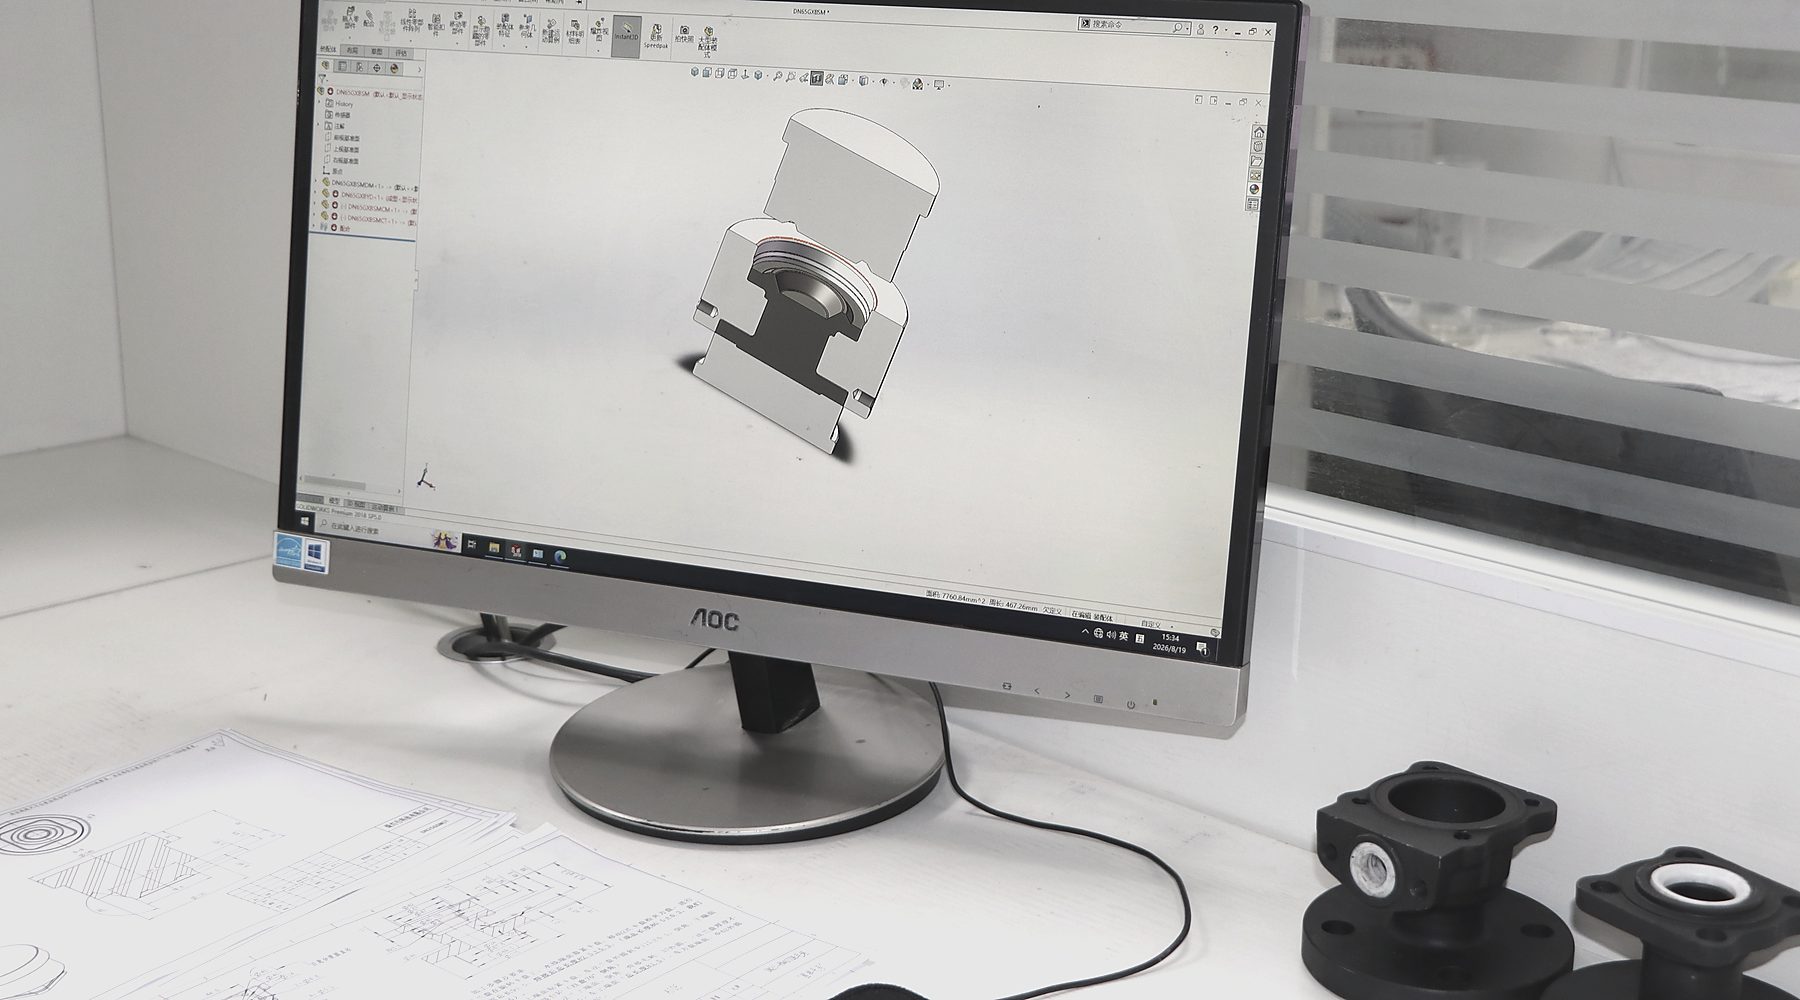
Tell us the size, the grade and the yearly quantity. You will get our comments on how the part forges, a tooling plan and a price for the blank.
- sales@ludonforge.com
- Telephone
- +41 78 218 18 94
- Works
- No. 11, Jingsi Road
Phoenix Industrial Park
Liaocheng, Shandong, China - Web
- ludonforge.com